Skip to content
▸ GOOD CHEMISTRY · WE MEAN BOTH KINDS
▸ TELEIOS / SAFETY & CORROSION
▸SAFETY & CORROSION · FOR POULTRY PROCESSORS

Same kill.
Easier on your people and your equipment.

Every intervention chemistry has a safety and maintenance profile, not just a kill rate. This page walks through what that means for your crew and your equipment, how T-24 compares to PAA and the other chemistries, and what changes when you switch.

02 ▸THE SAFETY SIDE

What your crew works
around today.

PAA works, and plants run it safely every day. But it asks a lot of the people beside it. The concentrate is a strong acid. At application points where crews work close to the chemistry, odor and irritation shape the PPE, the ventilation and, often, how high QA can set the dose.

02·A WHAT PAA ASKS OF YOUR CREW

The industry standard asks a lot of the people beside it.

Peracetic acid is the most widely used antimicrobial in U.S. poultry processing. It's a mixture of peracetic acid, hydrogen peroxide, and acetic acid, and the concentrate sits below pH 1. It's received, stored, and handled as a strong acid.

NIOSH classifies PAA as a strong sensory irritant. Exposure can irritate the eyes, skin, and respiratory tract [CDC NIOSH]. That's why every PAA program depends on PPE, ventilation, monitoring, and training at each application point.

▸ PAA · AT A GLANCE
CONCENTRATE pH < 1
HANDLED AS STRONG ACID · OXIDIZER
NIOSH STRONG SENSORY IRRITANT
CONTROLS PPE · VENTILATION · TRAINING
USE RULES USDA FSIS · 7120.1
▸ 02·B · THE SAFETY COST

Where the safety cost shows up.

The safety work around PAA is part of what you pay for when you run it. It just never shows up on the chemistry invoice.

It's also hard to plan around. The same dose setting can smell different from one shift to the next, because PAA's strength moves with water temperature, pH, organic load, and how it's measured [Unplucked podcast].

▸ Four places it lands
i.

THE CONCENTRATION CEILING

At application points where crews work close to the chemistry, how much odor people can tolerate often sets the dose, not the data.

ii.

THE SAFEGUARDS

PPE, ventilation, exposure monitoring, and training at every point PAA runs. Each one takes time and money.

iii.

THE COMPLAINT LOG

Odor and irritation complaints logged by safety, HR, and the plant nurse, often changing from shift to shift.

iv.

THE RETENTION NUMBERS

Hard-to-fill positions get harder to keep filled when the air on the line is part of the job.

None of this means PAA is unsafe. It means the safety work is real, ongoing, and worth putting into the decision.

02·C THE OTHER INTERVENTION CHEMISTRIES

How the other chemistries compare.

PAA isn't the only chemistry with a safety profile. Every option in the category asks something of the people who handle it. Here's how the common alternatives compare, so you can see where T-24 fits.

01 OXIDIZER

CHLORINE DIOXIDE

A strong oxidizer used in some food and water applications. Generated on-site and used in solution — gas-phase off-gassing and acid handling at the point of generation are the central safety concerns.

02 ACID + OXIDIZER

ACIDIFIED SODIUM CHLORITE

Activated with a GRAS organic acid (often citric) at the point of use, generating chlorous acid and chlorine dioxide. Brings both an acid-handling concern and an oxidizer concern.

03 OXIDIZER

CHLORINE

The poultry chiller workhorse before PAA replaced it in many plants. Lower-cost, with vapor concerns of its own and the chemistry of byproducts in organic-loaded water.

04 OXIDIZER

BROMINE COMPOUNDS

Used in some processing applications. Irritants, particularly to eyes and respiratory tract.

05 LOWER PROFILE

CPC + ORGANIC ACID

Generally lower in acute irritation profile, less common in high-volume poultry kill applications. Their own handling and labeling work.

03 ▸THE SAFETY SIDE, WITH T-24

What changes for your crew.

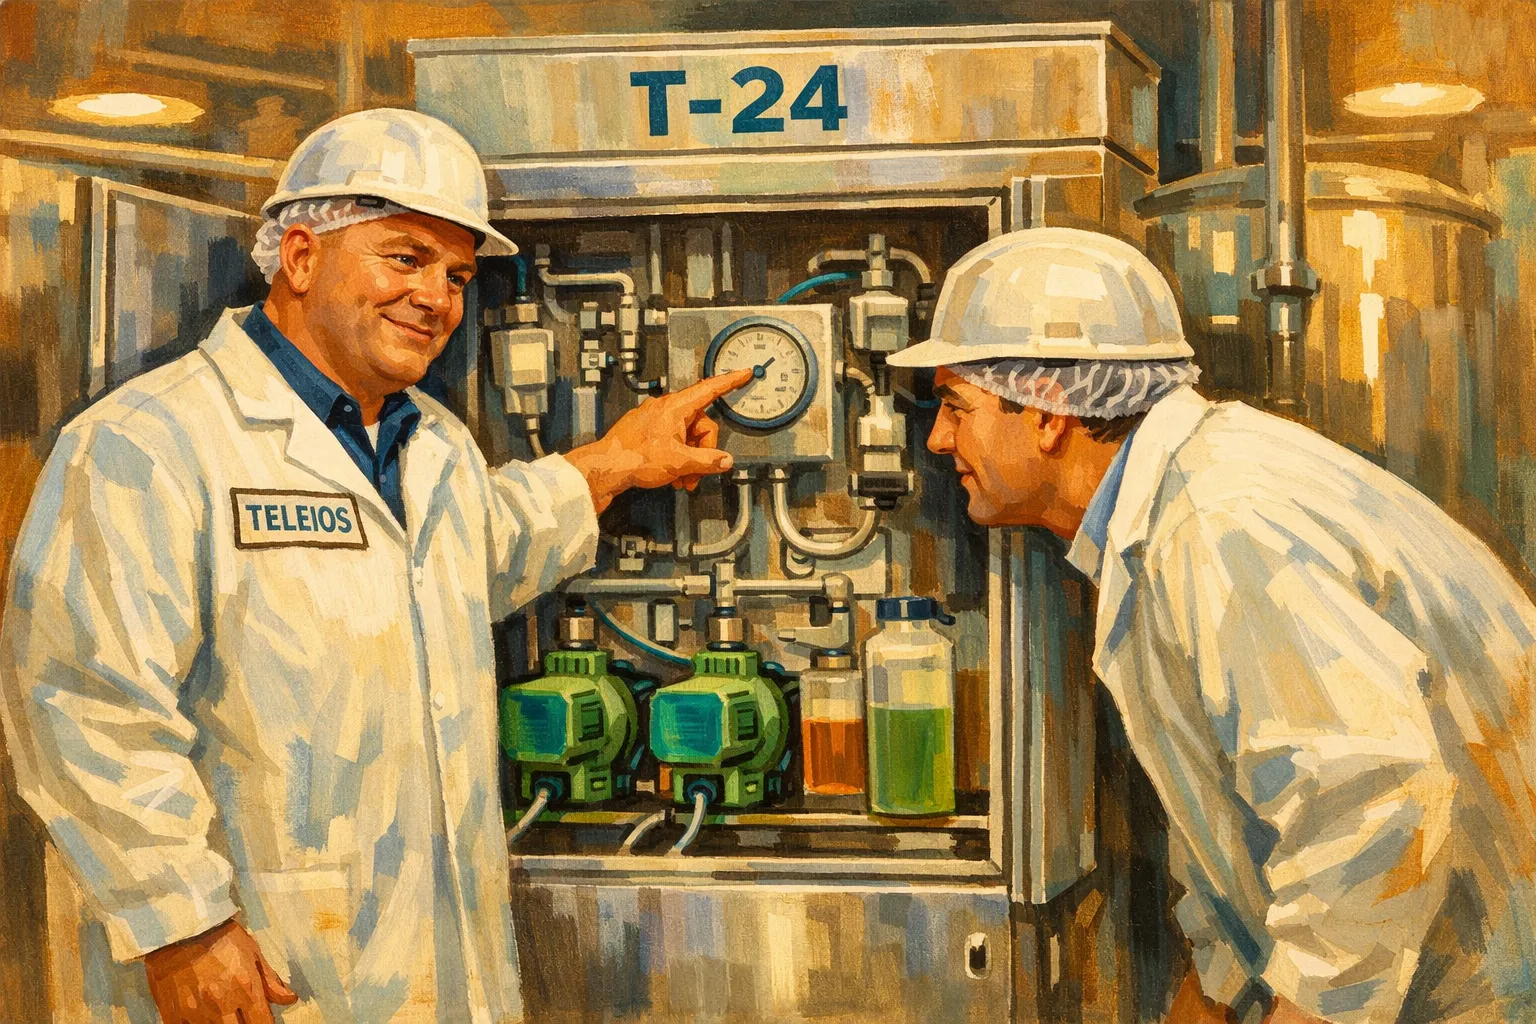
T-24 is a sodium peracetate antimicrobial generated on site from three ingredients. It changes the three things that drive the safety work around PAA: the odor, the acid, and the drums.

01 ▸ ODOR

Virtually odorless at use.

There's no vinegar smell at the application points. At the highest concentrations you may notice a faint ozone smell, and that's it.

Comfort stops setting the ceiling. QA can set the dose on the data at every point T-24 covers.
02 ▸ pH

Alkaline, not acidic.

At use, T-24 runs at pH 9 to 12, the opposite end of the scale from PAA.

There's no acid concentrate in the program for your crew to receive, pour, or work beside.

03 ▸ ON SITE

Made on site, as you need it.

The generator makes T-24 for your line as it runs.

No drums of concentrated PAA to receive, store, and transfer around the plant.

▸ WHAT YOU STILL HANDLE

On-site generation runs on three feedstocks: sodium hydroxide, hydrogen peroxide, and triacetin. Sodium hydroxide is caustic and hydrogen peroxide is an oxidizer, so both still need proper storage, PPE, and training. The difference is where the handling happens: at the generator, instead of acid concentrate at application points across the line.

04 ▸THE CORROSION SIDE

What the chemistry does
to your equipment.

Most intervention chemistries are acidic, strongly oxidizing, or both, and both wear metal over time. The damage builds slowly, and it almost never gets traced back to the chemistry that caused it.

04·A WHY IT HAPPENS

Two kinds of wear, in plain terms.

01

Acidic chemistries

▸ Acid attacks the metal.

Acid reacts directly with metal surfaces, and the lower the pH, the faster it works. Concentrated PAA sits below pH 1 and is still acidic at use. That's what wears stainless around dip tanks and spray cabinets, shortens the life of fasteners, and opens cracks in the concrete.

02

Oxidizing chemistries

▸ Oxidizers speed up rust.

Oxidizers speed up the same wear that air and water cause, just much faster. Chlorine, chlorine dioxide, bromine, hydrogen peroxide, and PAA all do this. Steel rated for normal plant water wears faster under a steady oxidizer load every shift.

03

PAA does both at once

▸ Acidic and oxidizing.

That's why corrosion shows up faster around PAA application points than anywhere else in the plant. Two kinds of wear on the same equipment, every shift. The maintenance log doesn't separate them. It just shows parts coming out ahead of spec.

04·B WHERE IT SHOWS UP

What a baseline walk usually finds.

  • ▸ METAL · DIP & SPRAY Metal around dip tanks and spray cabinets wearing faster than the engineering spec said it would.
  • ▸ FASTENERS · BRACKETS Fasteners and brackets in the spray zone that don't last their rated life.
  • ▸ CONCRETE Concrete cracks that open faster around application points than elsewhere in the plant.
  • ▸ DRAIN LINES Drain lines and floor drains wearing from a constant acid load.
  • ▸ CONVEYORS Nearby conveyor parts that catch overspray showing surface attack.

It's rarely one dramatic failure. It's a faster wear curve on everything the chemistry touches.

04·C WHO PAYS

Where the cost actually lands.

Corrosion costs get booked to maintenance, operations, and capital, never to the intervention chemistry that caused them.

A MAINTENANCE

Pays first. Labor, parts, and unscheduled repairs on shifts that didn't plan for them.

B OPERATIONS

Pays in downtime when a part has to come out ahead of spec.

C QA

Pays in uncertainty when worn equipment is harder to keep sanitary.

D LEADERSHIP

Pays in capital when a replacement lands on the budget months earlier than planned.

05 ▸THE CORROSION SIDE, WITH T-24

What changes for your equipment.

T-24 takes the acid out of the equation. It doesn't take corrosion off the table entirely, and we won't pretend it does.

▸ NO ACID LOAD

Alkaline at use.

T-24 runs at pH 9 to 12, so it doesn't put an acid load on the steel, fasteners, drains, and concrete around your application points. That removes one of the two kinds of wear PAA brings.

▸ MATERIALS TESTING

Less corrosion than PAA in testing.

In Clean Chemistry's materials testing, T-24 caused less corrosion than PAA on galvanized steel, carbon steel, copper, and brass.

▸ STRAIGHT TALK

Still an oxidant.

Every antimicrobial in this category is an oxidant, T-24 included. We don't claim T-24 stops corrosion. We claim it starts from a gentler place than an acidic chemistry, and we'll measure the difference on your equipment.

06 · NO TRADE-OFF

You don't give up kill to get there.

None of the safety or corrosion changes cost you microbial performance. In AEMTEK's red-water chiller simulation, T-24 delivered a 2.01 log₁₀ Salmonella reduction, on par with PAA. We validate it at your application points before anything changes.

Private-labeled for Teleios by Clean Chemistry, Inc. · Cleared under FDA FCN 2352 · Listed in USDA FSIS Directive 7120.1

2.01 log₁₀
▸ Salmonella reduction · chiller simulation
07 ▸WHAT CHANGES FOR YOUR TEAM

Every seat at the table.

Safety and corrosion don't land on one desk. Here's what each role deals with today, and what T-24 changes.

01

QA & Food Safety

▸ TODAY

Hitting micro targets at every intervention point, and defending the dose in an audit.

▸ WITH T-24

The same kill, with the dose set on the data instead of the smell, and a written record of what was actually run.

02

Safety · EHS

▸ TODAY

Odor and irritation complaints, PPE and ventilation demands, acid handling, and keeping hard-to-fill positions filled.

▸ WITH T-24

A virtually odorless, alkaline chemistry at the points T-24 covers, and no acid concentrate to handle on the line.

03

Maintenance

▸ TODAY

Steel, fasteners, drains, and concrete around the application points wearing out ahead of spec.

▸ WITH T-24

No acid load on the equipment T-24 touches, and a baseline to measure wear against.

04

Plant Manager · GM

▸ TODAY

Retention, downtime, and the costs that spread quietly across departments.

▸ WITH T-24

The chemistry's safety and corrosion costs pulled into one view, and measured at your plant.

08 ▸THE BASELINE WALK

Prove it in your plant.

Pick a day and we'll walk your application points with QA, safety, and maintenance. The answers to these six questions become the baseline a T-24 trial gets measured against. Not lab numbers. Your numbers.

01

Where do your operators notice odor or irritation most?

02

At which application points does comfort limit the concentration?

03

What PPE and ventilation does each application point require today?

04

What does maintenance replace sooner than spec near those points?

05

What have you spent on parts and concrete there in the last three years?

06

How fast does your supplier respond when something drifts?

▸ AFTER THE WALK

Then we stay.

Blue Ribbon Service keeps the program on track after installation: a weekly check-in with the same Teleios rep, and a written scorecard twice a month that safety, maintenance, QA, and the GM all see.

Book the Baseline Walk →
09 ▸THE THINGS THAT COME UP MOST

Three questions we hear most.

Short answers. Sourced where claims need sourcing.

Is PAA safe to use in poultry processing? +
PAA is widely used in poultry processing under USDA FSIS oversight as an approved antimicrobial processing aid. It can be effective. It also requires proper handling, monitoring, ventilation, training, and PPE because acute exposure can irritate the eyes, the respiratory tract, and the skin [CDC NIOSH].
Does T-24 stop corrosion? +
No chemistry in this category stops corrosion, and T-24 is still an oxidant. What changes is the acid. At pH 9 to 12, T-24 doesn't add the acid attack PAA brings, which removes one of the two ways PAA wears equipment. A baseline walk lets you measure the difference on your own equipment.
What does my crew still handle with on-site generation? +
The generator runs on three feedstocks: sodium hydroxide, hydrogen peroxide, and triacetin. Sodium hydroxide is caustic and hydrogen peroxide is an oxidizer, so both need proper storage, PPE, and training, as described in their safety data sheets. Your Teleios team reviews feedstock handling with EHS before installation.

▸ ALL CLAIMS ON THIS PAGE WITH AN EFFICACY, REGULATORY, OR HEALTH IMPLICATION CARRY A SOURCE OR ARE FLAGGED PENDING TECHNICAL REVIEW.

▸START HERE

Let's find out where we can help.

Odor, corrosion, a concentration ceiling, wastewater costs, slow service. Whatever is pushing your plant to look, we'll walk your line with your team, learn what matters most, and show you what T-24 and Blue Ribbon Service can change.